

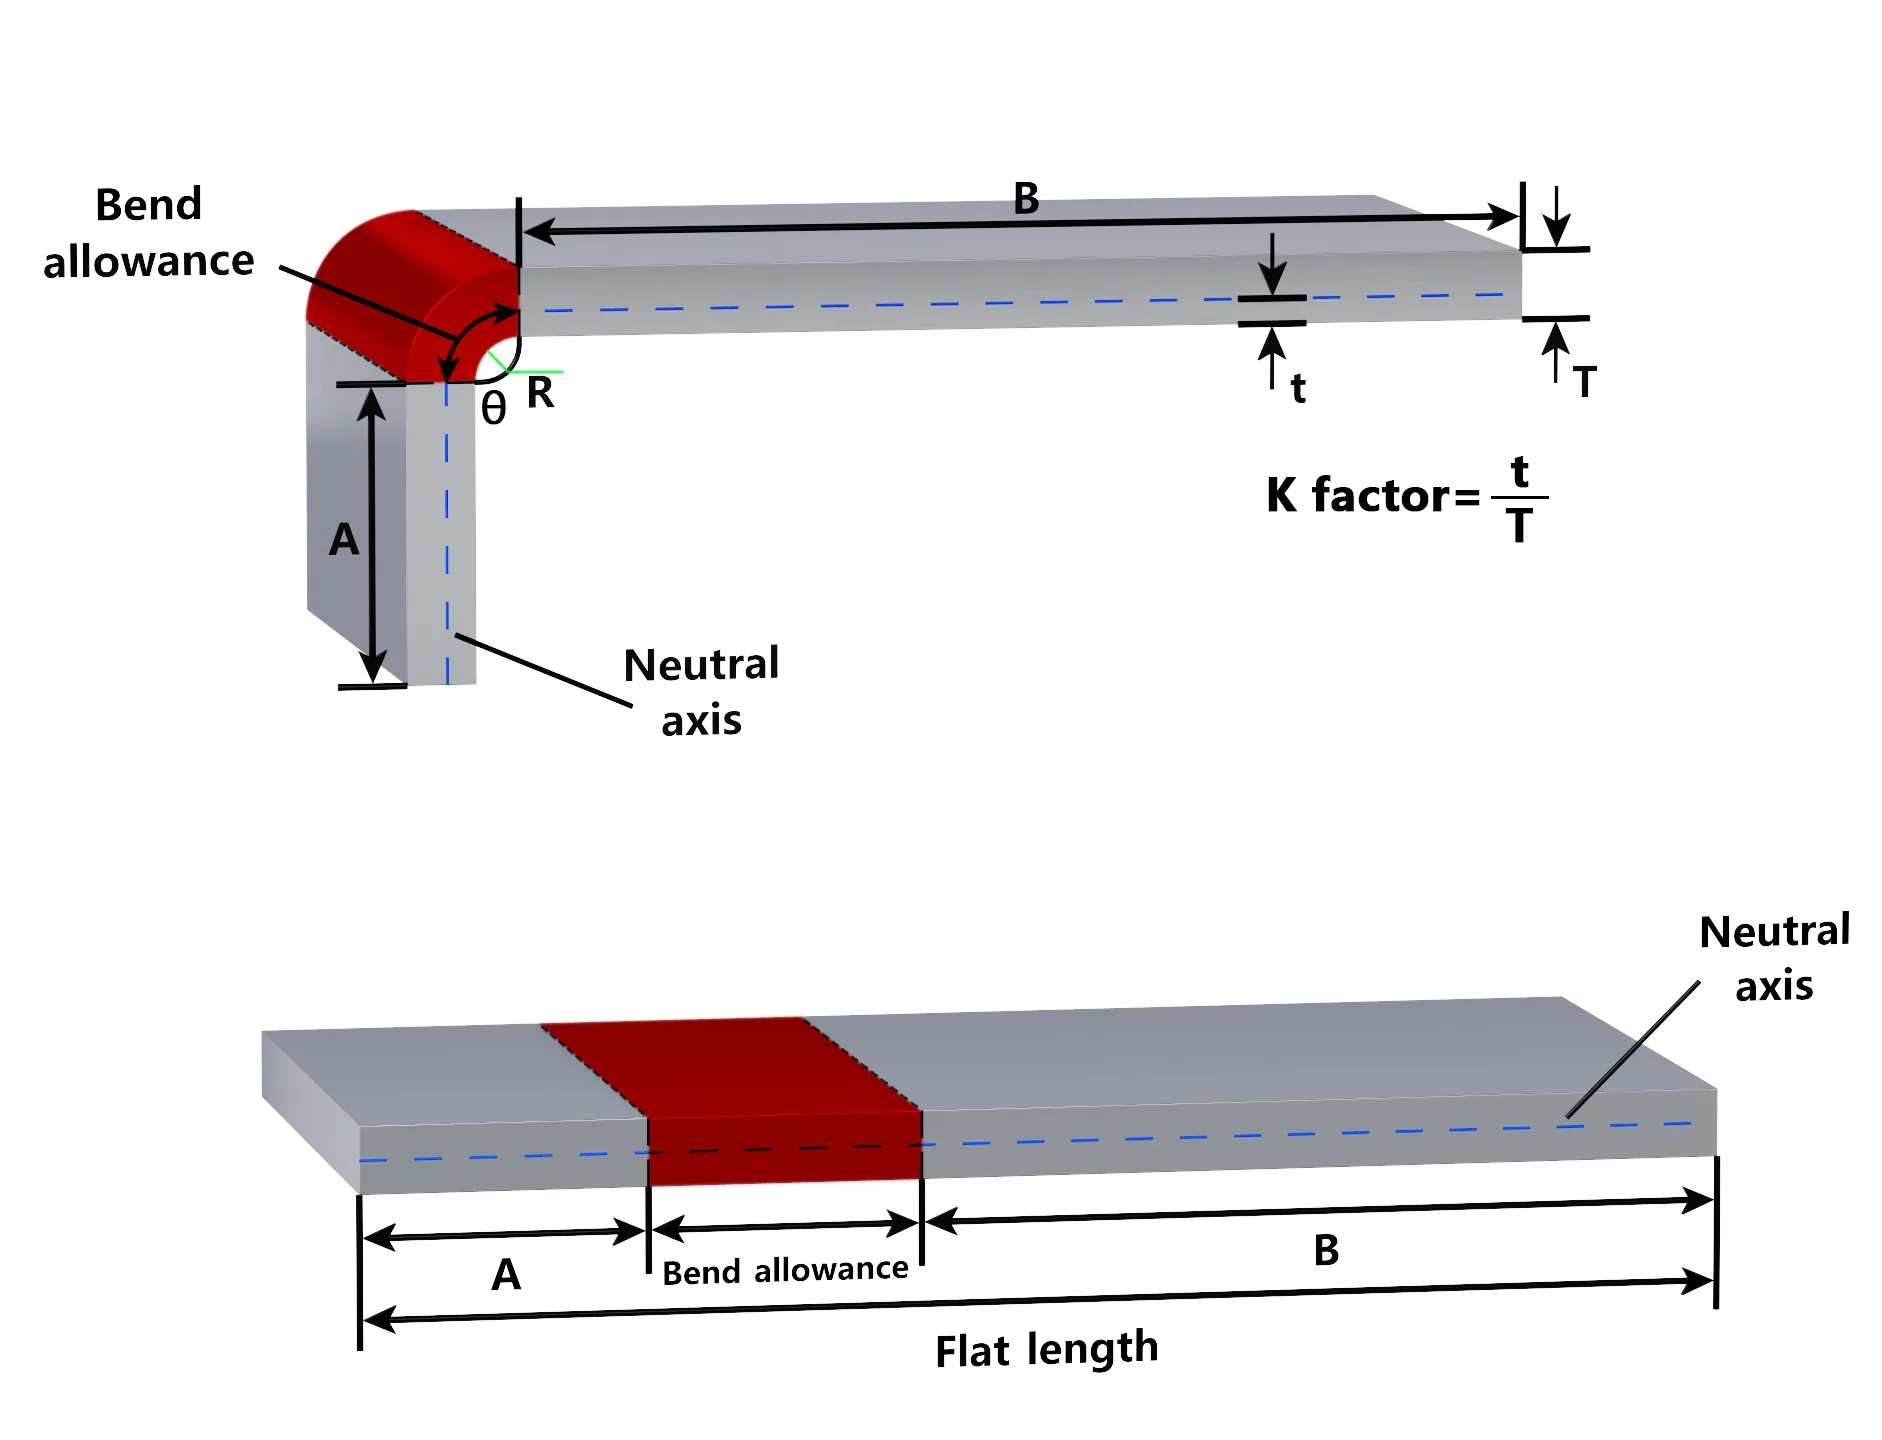
ال حاسبة بدل الانحناء gives the arc length of the bend along the neutral axis, so you can cut the flat blank to the right size. BA = π/180 × A × (R + K × T). A 90° bend in 2 mm sheet with a 2 mm inside radius has a bend allowance of 4.16 mm (K = 0.325). Enter your flange lengths to get the flat pattern length directly.
- Free, no sign-up
- Metric & imperial
- Instant results
- Shareable link
نتائج
LiveBend allowance (BA)Flat length 76.16 mm
- Flat blank length
- 76.16 mm
- Bend deduction (BD)
- 3.837 mm
- Outside setback (OSSB)
- 4.000 mm
- K-factor used
- 0.325 (DIN 6935)
- زاوية
- 90.0° bend · 90.0° included
K-factor “Auto” follows DIN 6935 (k = 0.65 + 0.5·log(R/T), K = k/2). For production, calibrate K with a test bend on your own tooling.
Bend allowance formula
BA = π / 180 × A × (R + K × T)A = bend angle in degrees (90° for an L-bracket)
Flat length L = A′ + B′ + BAA′, B′ = straight flange lengths up to the start of the bend (tangent points)
- بكالوريوس bend allowance – arc length of the neutral axis
- ر inside bend radius
- ت سمك المادة
- ك K-factor – neutral axis position as a fraction of T (0 to 0.5)
- أ bend angle (deflection), not the included angle
When your drawing shows outside (mold-line) dimensions, it is easier to subtract a bend deduction: L = A + B − BD, where BD = 2 × OSSB − BA and OSSB = tan(A/2) × (R + T). The calculator handles outside, inside and flat-leg dimensions automatically.
How to use the Bend Allowance Calculator
- أدخل سماكة و ال inside bend radius (for air bending, about 16% of the V-die opening).
- أدخل زاوية and say whether it is the bend angle or the included angle on the part.
- Leave the عامل K on Auto, or enter the value your shop has measured.
- Enter flange lengths أ و ب and how they are dimensioned to get the flat blank length.
Worked example
L-bracket, 2 mm mild steel, inside radius 2 mm, 90° bend, outside dimensions 50 × 30 mm.
- R/T = 1 → K = (0.65 + 0.5 × log 1) / 2 = 0.325
- BA = π/180 × 90 × (2 + 0.325 × 2) = 4.163 mm
- OSSB = tan 45° × (2 + 2) = 4.000 mm → BD = 2 × 4.000 − 4.163 = 3.837 mm
- Flat length L = 50 + 30 − 3.837 = 76.16 mm
Check: the straight legs are 46 mm and 26 mm, and 46 + 26 + 4.163 gives the same 76.16 mm.
K-factor chart (DIN 6935)
The K-factor locates the neutral axis inside the material. It depends mainly on the ratio of inside radius to thickness: tight bends push the neutral axis toward the inside (K ≈ 0.3), while gentle radii keep it in the middle (K = 0.5). Material type has a smaller effect — harder materials run slightly higher at the same R/T.
Typical air-bending values are 0.33 for mild steel, 0.40 for stainless steel and 0.38 for 5052 aluminum when R ≈ T.
| R / T | عامل K |
|---|---|
| 0.5 | 0.278 |
| 0.65 | 0.278 |
| 0.8 | 0.301 |
| 1 | 0.325 |
| 1.5 | 0.369 |
| 2 | 0.400 |
| 2.5 | 0.424 |
| 3 | 0.444 |
| 4 | 0.476 |
| ≥ 5 | 0.500 |
Bend allowance table for 90° bends
Inside radius equal to thickness, K-factor per DIN 6935. Values in mm.
| Thickness T | Radius R | عامل K | Bend allowance BA | Bend deduction BD |
|---|---|---|---|---|
| 1 | 1 | 0.325 | 2.08 | 1.92 |
| 1.5 | 1.5 | 0.325 | 3.12 | 2.88 |
| 2 | 2 | 0.325 | 4.16 | 3.84 |
| 3 | 3 | 0.325 | 6.24 | 5.76 |
| 4 | 4 | 0.325 | 8.33 | 7.67 |
| 5 | 5 | 0.325 | 10.41 | 9.59 |
| 6 | 6 | 0.325 | 12.49 | 11.51 |
| 8 | 8 | 0.325 | 16.65 | 15.35 |
| 10 | 10 | 0.325 | 20.81 | 19.19 |
Frequently asked questions
What is bend allowance in sheet metal?
Bend allowance is the length of the neutral axis through the bend. It is the material you must add to the two straight flange lengths to get the flat blank length: L = A′ + B′ + BA.
What is the difference between bend allowance and bend deduction?
Bend allowance is added to the straight (tangent) flange lengths; bend deduction is subtracted from the outside (mold-line) dimensions. Both give the same flat length. Use whichever matches how your drawing is dimensioned.
What K-factor should I use?
Use about 0.33 for air bending mild steel with R ≈ T, 0.40–0.45 for larger radii and 0.5 when R is more than five times T. The most accurate K-factor comes from measuring a test bend on your own press brake and tooling.
Do I enter the bend angle or the included angle?
The formula uses the bend angle — how far the flange is bent from flat (90° for an L-bracket). If your drawing shows the included angle between the flanges, select “Included angle” and the calculator converts it (bend angle = 180° − included angle).
How does the inside radius affect the flat length?
A larger inside radius makes the bend allowance longer and the bend deduction smaller. In air bending the radius is set by the V-die (about 16% of V for mild steel), not by the punch tip, so use the radius you will actually get.
Reviewed by the HARSLE engineering team · Last updated October 2026. Results are engineering estimates; confirm critical values with your machine and tooling documentation.
Bend allowance (BA)—


