

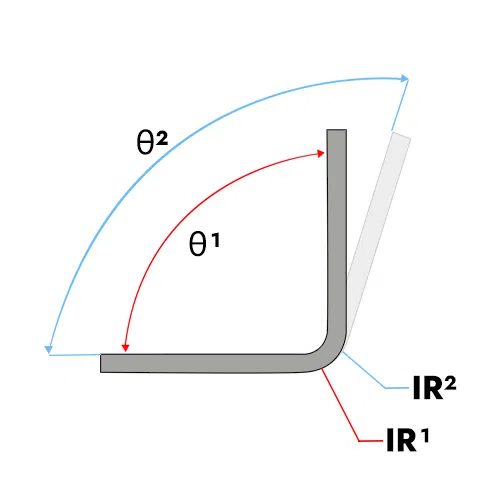
O spring back calculator tells you how far to overbend so the part relaxes to the angle you need. It uses the classic springback equation Ri/Rf = 4x³ − 3x + 1 with x = Ri·Y/(E·t). Example: 2 mm 6061-T6 aluminum bent over a 20 mm radius springs back 11.7°, so you must bend to 101.7° to finish at 90°.
- Free, no sign-up
- Metric & imperial
- Instant results
- Shareable link
Resultados
LiveBend to (overbend angle)bend to this angle to finish at 90.0°
- Springback angle
- 11.66°
- Springback factor Ks
- 0.8853
- Final inside radius
- 22.721 mm
- Included angle to program
- 78.34° (target 90.0°)
- Radius / thickness
- 10.00
Theoretical elastic springback (Gardiner). Real springback also depends on die width, grain direction and material batch — confirm with a test bend.
Springback formula
Ri / Rf = 4x³ − 3x + 1, with x = Ri × Y / (E × t)Ri initial radius · Rf final radius · Y yield strength · E elastic modulus · t thickness
Ks = αf / αi = (Ri + t/2) / (Rf + t/2)αi = angle bent on the machine · αf = angle after release
Springback grows with the radius-to-thickness ratio e o yield-to-modulus ratio. That is why high-strength steel, titanium and hard aluminum spring back far more than mild steel or copper, and why large-radius bends are much harder to hold than tight ones. For tight air bends (R < 3t) the elastic formula underestimates; the calculator then also shows the typical shop range for the material.
How to use the Spring Back Calculator
- Selecione o material (or enter yield strength and modulus from the certificate).
- Digitar grossura e o inside radius you are forming.
- Entre no target angle you need after the part is released.
- Program the press brake to the overbend angle, then fine-tune after the first part.
Worked example
2 mm aluminum 6061-T6, 20 mm radius, target 90°.
- x = 20 × 276 / (69,000 × 2) = 0.040
- Ri/Rf = 4 × 0.040³ − 3 × 0.040 + 1 = 0.880 → Rf = 22.72 mm
- Ks = (20 + 1) / (22.72 + 1) = 0.885
- Bend to 90 / 0.885 = 101.7° → springback 11.7°
The same bend in mild steel springs back only about 3.2°.
Material data and typical springback
| Material | Yield Y (MPa) | Modulus E (GPa) | Typical air-bend springback at 90°, R ≈ t |
|---|---|---|---|
| Mild steel S235 / A36 | 250 | 207 | 0.5–1.5° |
| Structural steel S355 | 355 | 207 | 1–2.5° |
| High-strength steel S700 | 700 | 207 | 3–6° |
| Aço inoxidável 304 | 260 | 193 | 2–3.5° |
| Aluminum soft (1100-O) | 35 | 69 | 0.5–1° |
| Aluminum half hard (3003-H14) | 130 | 69 | 1–2° |
| Alumínio 5052-H32 | 195 | 70 | 1.5–3° |
| Alumínio 6061-T6 | 276 | 69 | 3–6° |
| Copper soft | 70 | 117 | 0.3–1° |
| Copper half hard | 200 | 117 | 1–2° |
| Latão | 300 | 100 | 1–2° |
| Titânio Grau 2 | 345 | 105 | 4–8° |
Frequently asked questions
What is springback in sheet metal bending?
Springback is the elastic recovery of the sheet when the bending force is released: the angle opens and the radius grows. You compensate by overbending so the part relaxes to the angle you need.
How much does stainless steel spring back?
In a tight air bend (R ≈ t), 304 stainless typically springs back 2–3.5° at 90°, roughly twice as much as mild steel. With larger radii the springback rises quickly, as the formula shows.
Why do large radius bends spring back more?
A larger radius means less of the cross-section is plastically deformed, so a bigger share of the bend is elastic and recovers. Springback rises roughly with R/t.
How can I reduce springback?
Use a tighter radius or narrower V-die, bottom or coin the bend, overbend with CNC angle correction, choose a softer temper, or bend across the rolling direction. CNC press brakes with angle measurement compensate automatically.
What is the springback factor Ks?
Ks is the ratio of the final angle to the bent angle. Ks = 1 means no springback; Ks = 0.95 means a part bent to 94.7° relaxes to 90°.
Reviewed by the HARSLE engineering team · Last updated October 2026. Results are engineering estimates; confirm critical values with your machine and tooling documentation.
Bend to (overbend angle)—


