

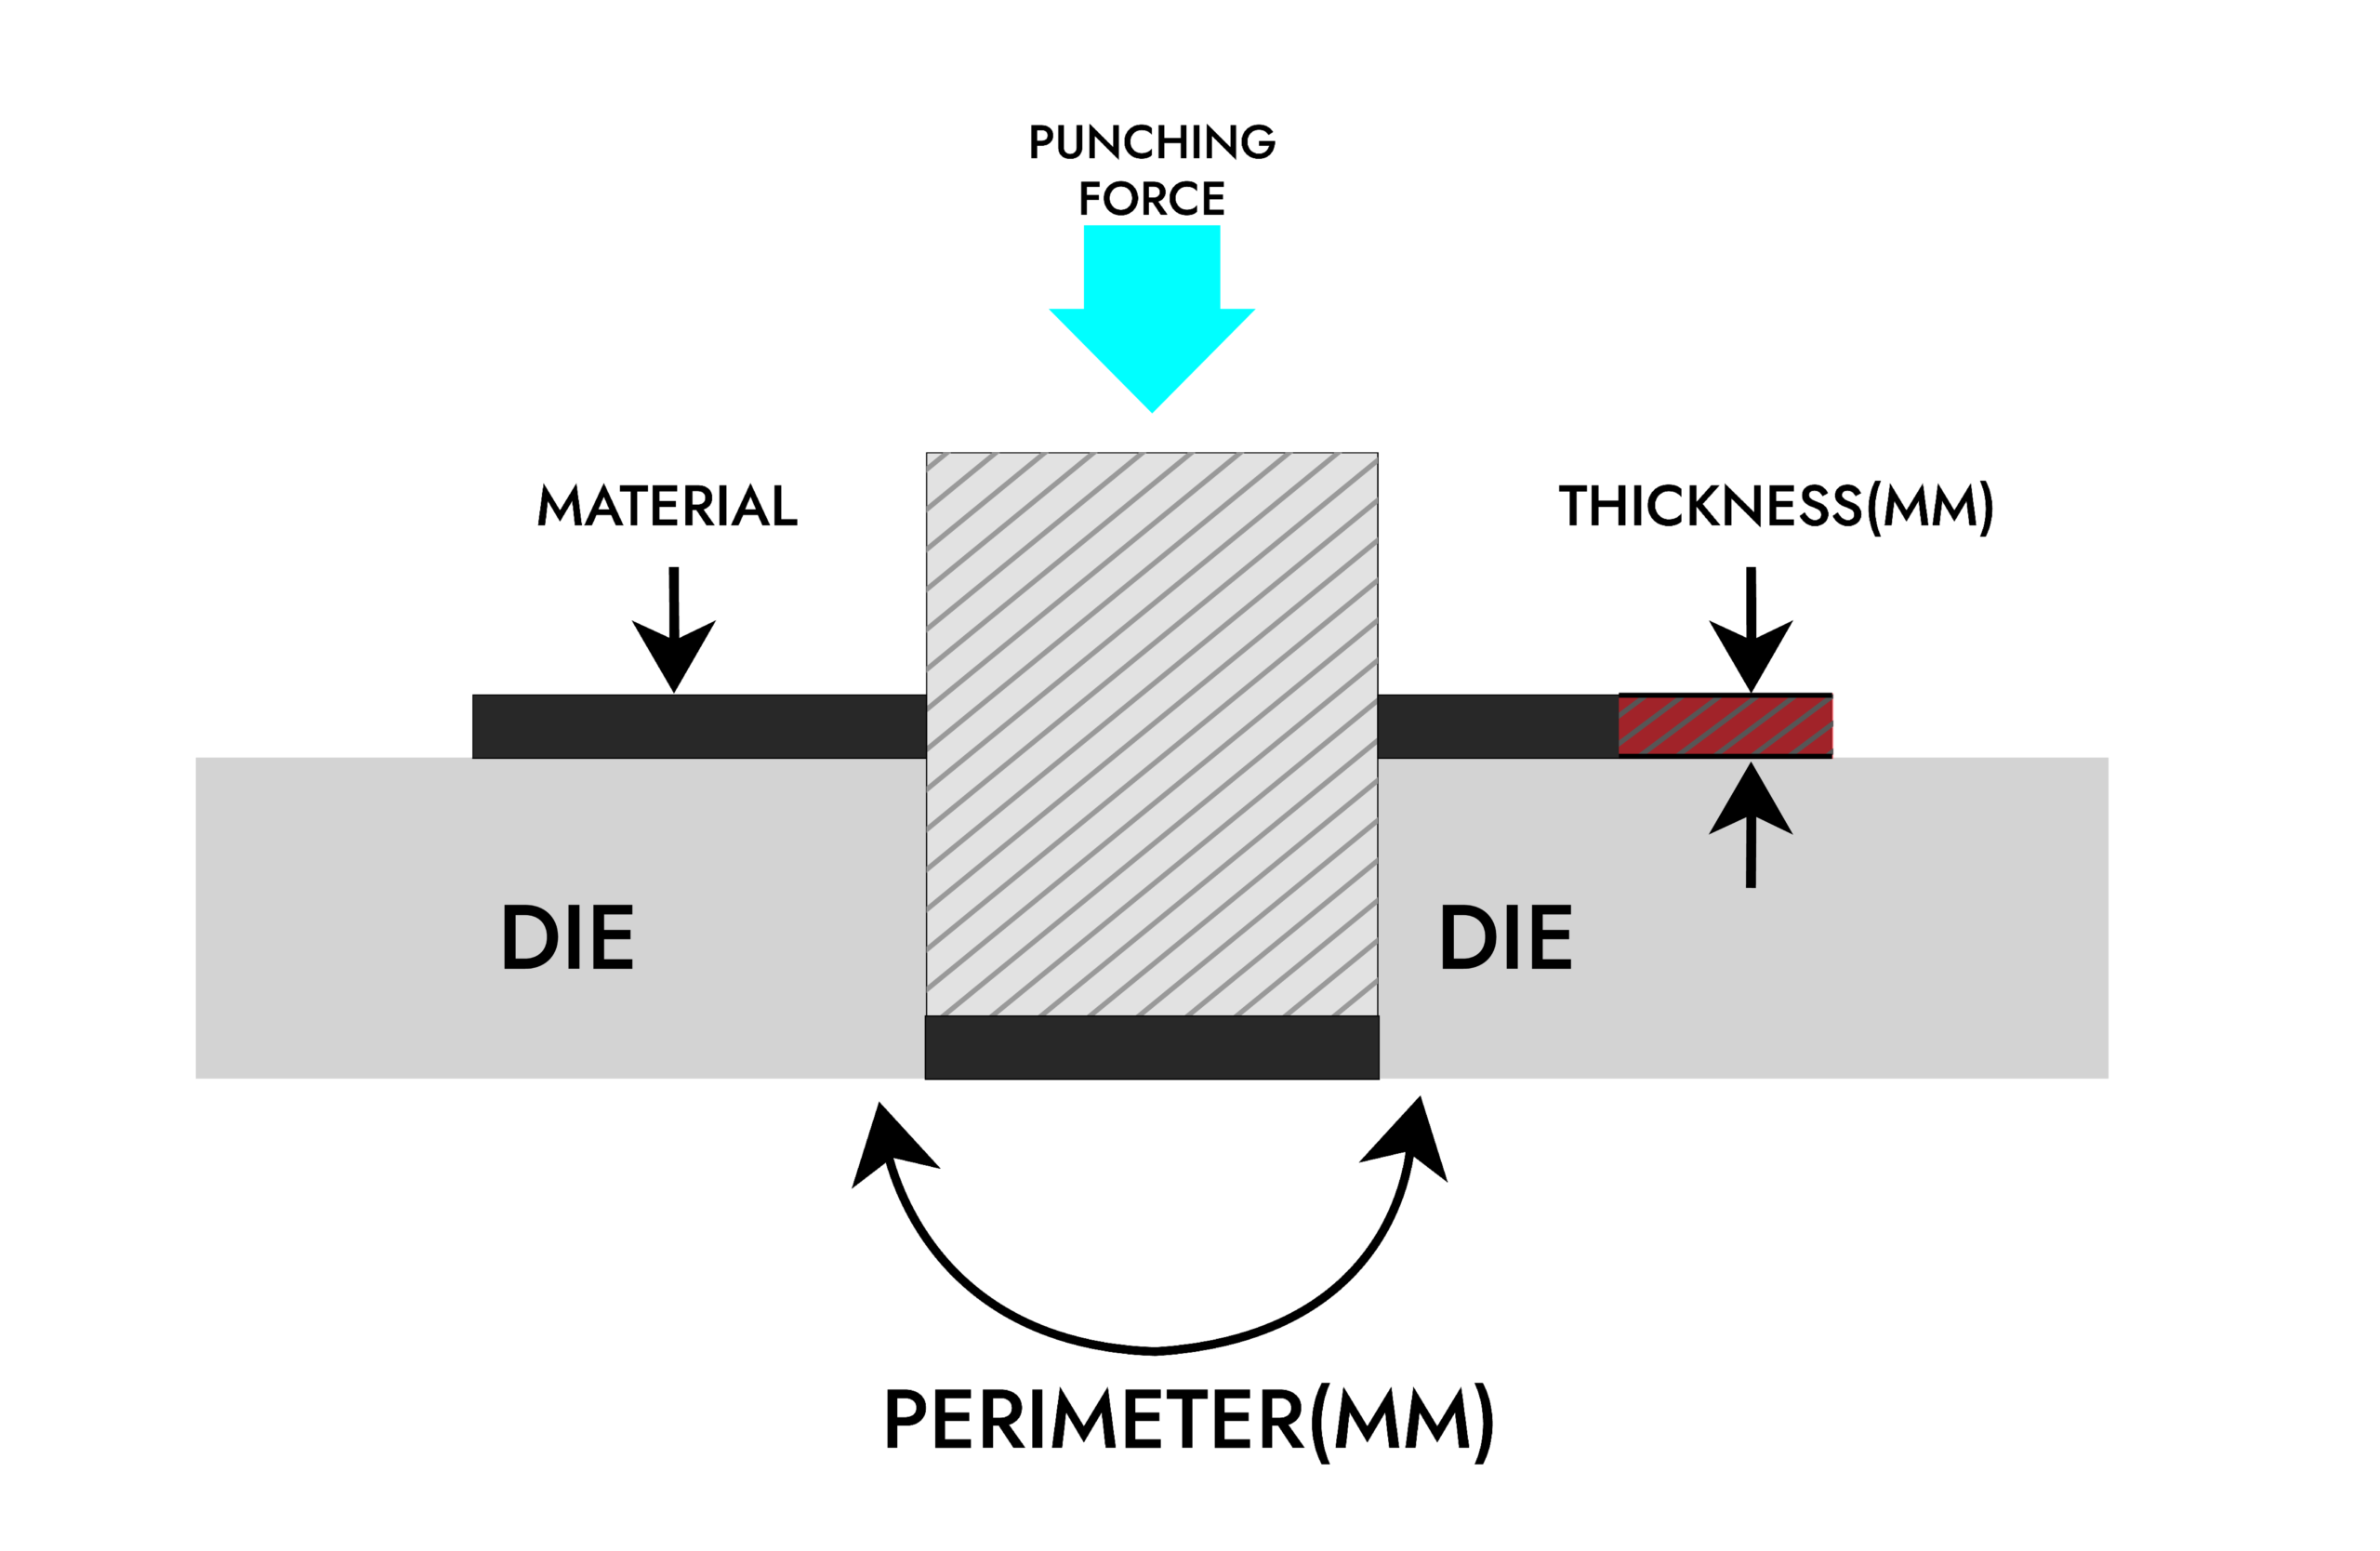
Der Stanzkraftrechner works out the tonnage needed to punch a hole: F = perimeter × thickness × shear strength. A Ø20 mm hole in 3 mm mild steel needs 65 kN (6.6 T). The calculator handles round, square, rectangular, slotted and hexagonal punches and also gives the right punch-to-die clearance.
- Free, no sign-up
- Metric & imperial
- Instant results
- Shareable link
Ergebnisse
LivePunching force65.0 kN · 7.31 US tons
- Force (kN)
- 65.0 kN
- Cut perimeter
- 62.83 mm
- Die clearance
- 0.750 mm total (25% of t)
- Clearance per side
- 0.375 mm
- Die diameter
- 20.75 mm
Clearance follows common turret-punch tooling practice (total clearance as % of thickness). Shear strength τ ≈ 0.8 × tensile strength.
Punching force formula
F = L × t × τF in N · L cut perimeter in mm · t thickness in mm · τ shear strength in MPa
- L perimeter of the punch: π·d (round), 4a (square), 2(a+b) (rectangle), 2(a−b)+π·b (slot), 3.46·s (hexagon across flats)
- T Blechdicke
- τ shear strength (about 80% of the tensile strength)
Divide newtons by 9,807 for metric tons. Add about 30% for punch wear and material variation. Shear-angle (roof-top) punches reduce the peak force by 30–50% on thick material. Stripping force is usually 5–10% of the punching force.
How to use the Punching Force Calculator
- Wählen Sie die Material.
- Geben Sie den Blechdicke.
- Wählen Sie das Symbol punch shape and enter its dimensions.
- Enter the number of holes per hit for multi-tools, then read the force and clearance.
Worked example
Ø20 mm hole in 3 mm mild steel. L = π × 20 = 62.83 mm → F = 62.83 × 3 × 345 = 65,031 N = 65.0 kN (6.63 T). With a 30% margin choose at least 8.6 T. Die clearance 25% of 3 mm = 0.75 mm total (0.375 mm per side) → die Ø20.75 mm.
Punching force chart – mild steel (metric tons, T)
Round holes, τ = 345 MPa. Columns: sheet thickness in mm.
| Hole | 1 mm | 2 mm | 3 mm | 4 mm | 6 mm |
|---|---|---|---|---|---|
| Ø5 | 0.55 | 1.11 | 1.66 | 2.21 | 3.32 |
| Ø10 | 1.11 | 2.21 | 3.32 | 4.42 | 6.63 |
| Ø20 | 2.21 | 4.42 | 6.63 | 8.84 | 13.26 |
| Ø30 | 3.32 | 6.63 | 9.95 | 13.26 | 19.89 |
| Ø50 | 5.53 | 11.05 | 16.58 | 22.10 | 33.16 |
Punch–die clearance guide (total, % of thickness)
| Material | Thin | Medium | Thick |
|---|---|---|---|
| Aluminum, copper, brass | 15% (< 2.5 mm) | 20% (2.5–5 mm) | 25% (> 5 mm) |
| Mild / galvanized steel | 20% (< 3 mm) | 25% (3–6 mm) | 30% (> 6 mm) |
| Stainless / high-strength steel | 20–25% (< 2.8 mm) | 30% (2.8–4 mm) | 35% (> 4 mm) |
Frequently asked questions
How do you calculate punching tonnage?
Multiply the cut perimeter by the sheet thickness and the material shear strength: F = L × t × τ. In metric tons for mild steel: perimeter (mm) × thickness (mm) × 0.0352. A Ø20 mm hole in 3 mm steel is 62.8 × 3 × 0.0352 ≈ 6.6 t.
What is the smallest hole I can punch?
As a rule the punch diameter should be at least equal to the sheet thickness for mild steel and 1.5–2 times the thickness for stainless steel. Smaller punches tend to buckle or break.
What die clearance should I use?
Total clearance of about 20–25% of thickness for mild steel, 15–20% for aluminum and 25–35% for stainless steel. Correct clearance lowers the force, reduces burr and extends punch life.
How can I reduce punching force?
Use a shear-angle (roof-top or whisper) punch, stagger tools so they do not cut at the same time, punch a smaller pre-hole, or use a machine with more tonnage.
Reviewed by the HARSLE engineering team · Last updated October 2026. Results are engineering estimates; confirm critical values with your machine and tooling documentation.
Punching force—


