

Industry Solutions · Elevator Doors & Cabins
Sheet Metal Machines for Elevator Door & Cabin Panel Manufacturing
Long, flat and flawless — machines for stainless steel landing doors, car doors and cabin wall panels.
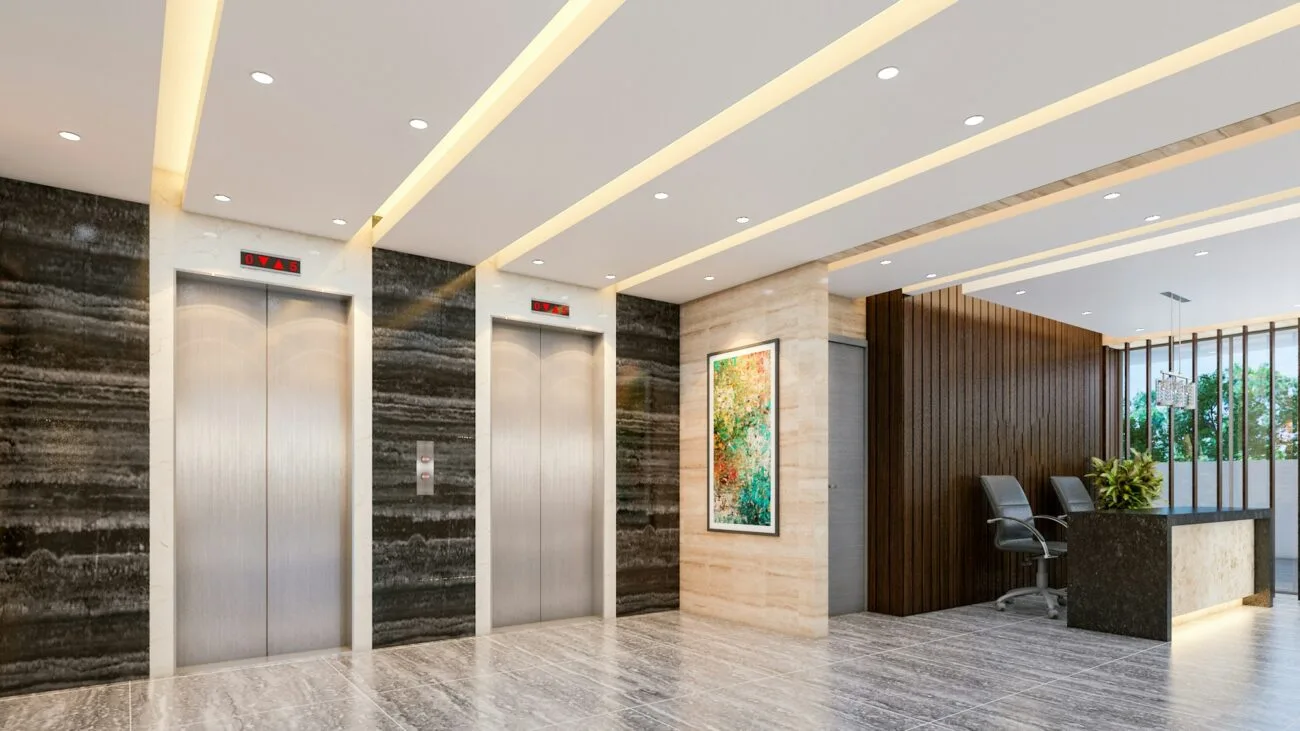
Elevator Manufacturing Basics
How Elevator Doors & Cabins Are Made
Elevator doors and cabin panels are long stainless steel or coated steel panels (typically 1.0–1.5 mm, 2–3 m long) with decorative surfaces. They are cut by shear or fiber laser, V-grooved where a sharp edge is required, folded on a panel bender or long CNC press brake, then laser welded and finished without marking the visible face.
Surface protection drives the whole process: hairline and mirror stainless must not be scratched or dented, flanges must be parallel over the full length, and the stiffening ribs on the back are welded with minimal heat marks.
Typical Parts & Materials
- Landing doorsLong panels with return flanges and stiffenersStainless steel / coated steel 1.0–1.5 mm
- Car doorsSharp-edged, decorative visible faceHairline or mirror stainless 1.0–1.5 mm
- Cabin wall panelsLarge flat panels, tight flatnessStainless steel 1.0–1.5 mm
- Door frames & jambsLong multi-bend profilesStainless / galvanized steel 1.2–2.0 mm
- Ceilings & kick platesPerforated or embossed panelsStainless / aluminum 0.8–1.5 mm
Manufacturing Process
From Flat Sheet to Finished Part
Select a stage to see what happens and which HARSLE machines do the work.
Étape 1Elevator Doors & Cabins
Cutting & Blanking
Shears and fiber lasers cut long blanks; V-grooving machines cut a groove on the bend line so stainless edges stay sharp and decorative.
Machine à cisailler
43 models in the HARSLE range.
Machine de découpe laser
60 models in the HARSLE range.
Machine à rainurer en V
12 models in the HARSLE range.
Machine à entailler
15 models in the HARSLE range.
Étape 2Elevator Doors & Cabins
Bending & Forming
Panel benders fold long doors without lifting the sheet; long-bed or tandem CNC press brakes form frames and jambs.
Cintreuse de panneaux
25 models in the HARSLE range.
Presse plieuse
196 models in the HARSLE range.
Étape 3Elevator Doors & Cabins
Welding & Finishing
Laser welding fixes stiffeners and corners with minimal heat tint; deburring and polishing protect the visible surface.
Machine de soudage laser
21 models in the HARSLE range.
machine à ébavurer
30 models in the HARSLE range.
Étape 4Elevator Doors & Cabins
Automation & Tooling
Panel flippers and tooling with protective films reduce handling marks on decorative sheets.
Panneau rabattable
9 models in the HARSLE range.
Outillage
22 models in the HARSLE range.
Recommended Machines
Machines for Elevator Doors & Cabins
Live from the HARSLE product range — models suited to elevator manufacturing are listed first.
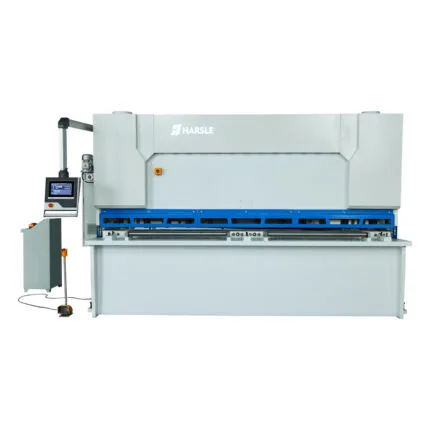
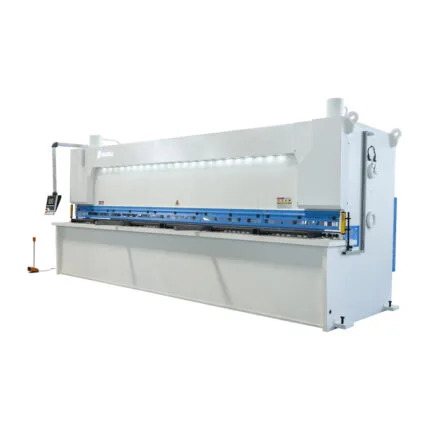
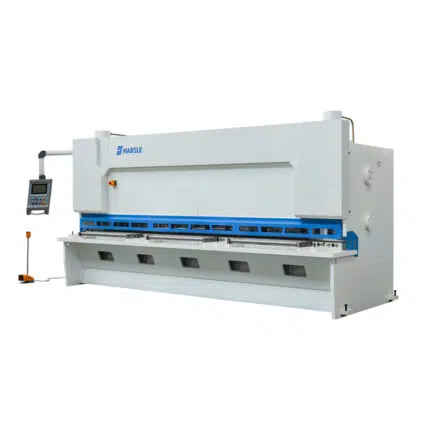
 Cisaille à guillotine PrimeShear 1232 DAC360TPrimeShear 1232 DAC360T is a high-performance CNC guillotine shearing machine designed for accurate and efficient sheet metal cutting.…View details
- Cisaille guillotine PrimeShear 1260 de haute précisionThe PrimeShear 1260 Guillotine Shear is designed for high precision and efficient sheet metal cutting. Built for industrial…View details
- HARSLE PrimeShear 1240 avec DAC360 ControlThe PrimeShear 1240 with DAC360 system from HARSLE is a high-performance guillotine shearing machine designed for precision metal…View details
- Cisaille hydraulique PrimeShear 0632 avec système anti-torsionThe PrimeShear 0632 is a high-performance hydraulic shearing machine designed for precise and stable sheet metal cutting. Equipped…View details
- Machine de cisaillement de haute précision pour l'industrie automobileA shearing machine for automotive industry is designed for high-precision cutting of steel, aluminum, and alloy sheets used…View details
- Machine de cisaillement de tôles épaisses pour la découpe de métaux lourdsThe thick plate shearing machine is designed for high-strength and large-thickness metal sheet cutting in heavy industrial applications.…View details
- Machine de découpe laser haute précision de 20 kW pour l'industrieThe 20kw laser cutting machine delivers high‑power precision cutting for various metals, including steel, aluminum, and stainless steel.…View details
- Machine de découpe laser 4 kW pour la fabrication de métauxThe 4kW Laser Cutting Machine is designed for high-speed, high-precision metal processing. Equipped with advanced fiber laser technology,…View details
- Machine de découpe laser haute précision pour feuilles mincesThis laser cutting machine for thin sheets delivers precise, fast, and clean cuts for a variety of metal…View details
- Machine de découpe laser à fibre de 12 kW pour métauxThe 12kW Fiber Laser Cutting Machine is designed for high-speed, high-precision metal processing. Equipped with advanced fiber laser…View details
- Machine de découpe laser de tubes métalliques de 3 kWThe 3kW Laser Tube Cutting Machine is designed for high-speed and high-precision cutting of metal tubes and pipes.…View details
- Machine de découpe laser pour le traitement de l'acier inoxydableHARSLE laser cutting machine for stainless steel is designed for high-speed, high-precision metal processing. It delivers clean cutting…View details
- Machine à rainurer les métaux de haute précision pour la fabrication de tôlesThe HARSLE Metal Grooving Machine is designed for high-precision V-grooving on stainless steel, aluminum, and other sheet materials.…View details
- Machine à rainurer horizontale EcoGroove 4012 pour la précisionThe EcoGroove 4012 Horizontal Grooving Machine is designed for precise and efficient sheet metal grooving. With a processing…View details
- Meilleurs fournisseurs de machines à rainurer en V pour des coupes de précisionFind top V Grooving Machine Suppliers offering high-quality, precise cutting solutions for sheet metal fabrication. Our V grooving…View details
- Trouvez dès aujourd'hui le meilleur prix pour une machine à rainurer en V.V Groove Cutter Machine Price is crucial for businesses looking to optimize metal cutting. HARSLE offers high-precision, cost-effective…View details
- Machine à rainurer en V verticale à coût élevé et à haut rendementThe high cost efficient vertical V grooving machine is designed for precision V-grooving in sheet metal fabrication. It…View details
- Machine à rainurer en V haute efficacité pour tôlesThe V Grooving Machine for Sheet Metal is designed for high precision grooving and bending, offering clean, accurate…View details
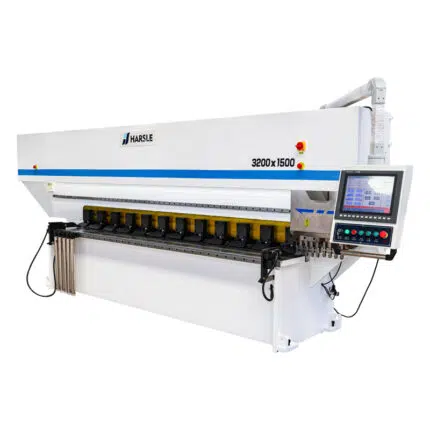
- Machine de découpe à encoches en V pour tôles décorativesThe V Notch Cutting Machine is designed for precise grooving and trimming of stainless steel, aluminum, and other…View details
- Fraise à angle fixe pour la découpe de précision des métauxThe Fixed Angle Cutter for Metal is designed for precise and efficient cutting of various metals at fixed…View details
- Machine à encocher à angle fixe pour découpe de précisionThe Fixed Angle Notcher Machine is designed for precise cutting and notching of sheet metal at fixed angles.…View details
- Encocheuse en aluminium à angle réglableHARSLE Aluminum Notching Machine is designed for precise and efficient corner cutting of aluminum sheets and profiles. With…View details
- Travaux de machines de premier ordre Équipement de tôlerieHARSLE Top Notching Machine Works Sheet Metal Equipment delivers high precision, reliability, and efficiency for all your metal…View details
- Encocheuse à haute efficacité pour la coupe de tuyauxThe HARSLE Notching Machine for Pipe offers precise, efficient, and consistent notching for round, square, or rectangular tubes.…View details
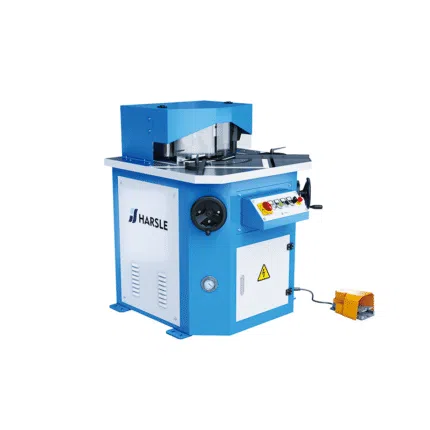
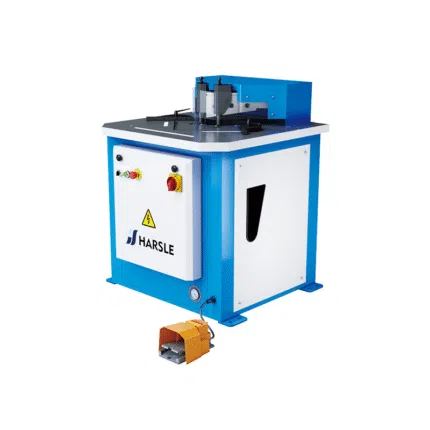
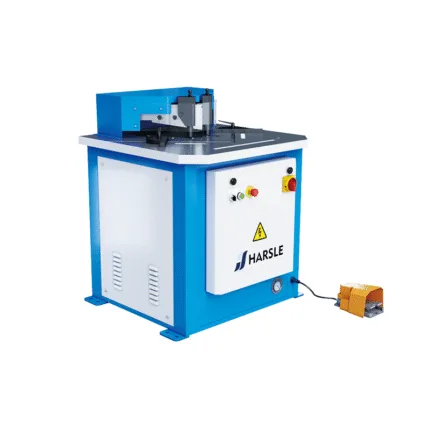
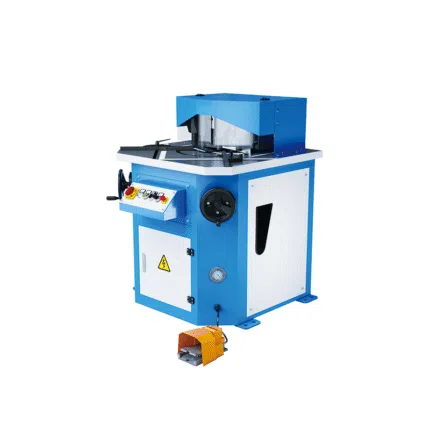
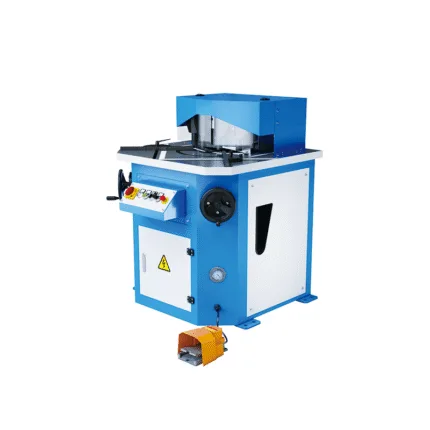
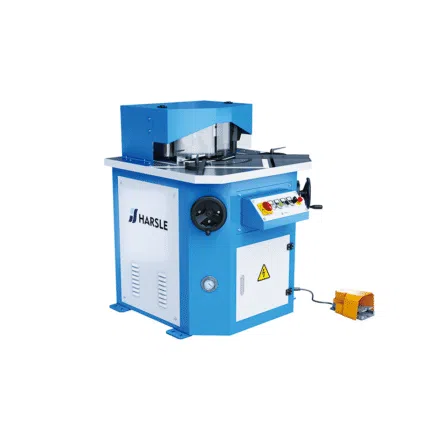
- Cintreuse de panneaux CNC pour le formage de panneaux d'ascenseurThe Panel Bender for Elevator Panels from HARSLE provides high-precision, automated bending solutions for stainless steel and decorative…View details
- AutoBend 2500 Ultra avec changement d'outil automatiqueThe AutoBend 2500 Ultra is an advanced panel bending solution featuring Auto Tool Change technology for faster, more…View details
- Poste de travail robotisé automatisé de pliage de tôles pour une précision optimaleThis Automated Robotic Sheet Metal Bending Workstation delivers fast, precise, and fully automated bending for modern fabrication shops.…View details
- Cellule de pliage robotisée intelligente pour la production d'armoiresThis Robotic Smart Bending Cell for Cabinet Production is an advanced automated bending solution designed for high-precision, high-efficiency…View details
- Solution de pliage de panneaux robotisée industrielle pour la fabrication intelligenteThis Industrial Robotic Panel Bending Solution is engineered for manufacturers seeking higher precision, faster throughput, and fully automated…View details
- Cellule de pliage robotisée intelligente pour tôles intelligentesThe Intelligent Robotic Bending Cell is a fully automated sheet metal bending solution designed for high precision, consistent…View details
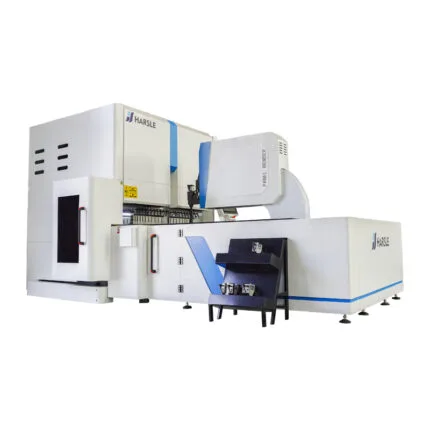
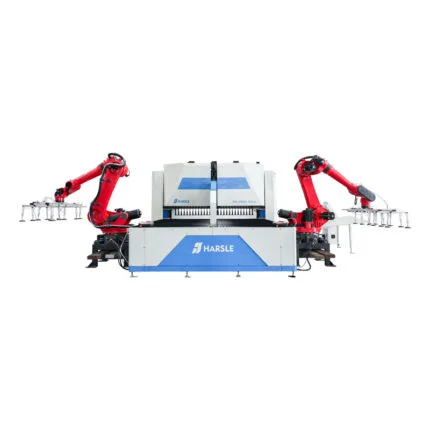
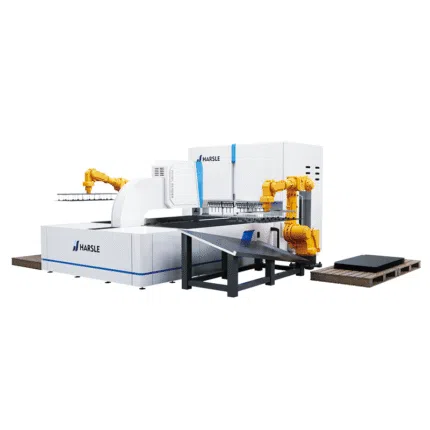
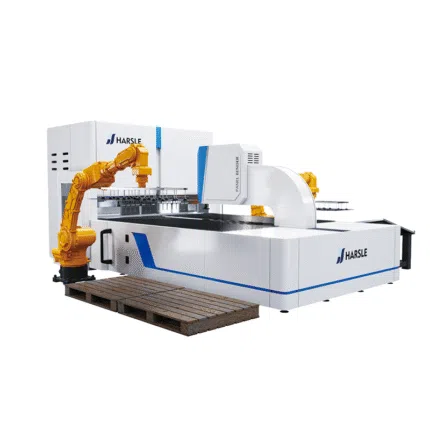
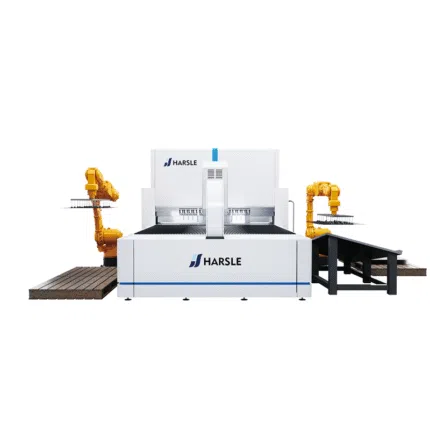
- MegaBend 80060 Heavy Duty Press Brake With DA66SThe MegaBend 80060 Heavy Duty Press Brake is engineered for high-capacity and large-format sheet metal bending applications. With…View details
- E-Bend 3512 Servo Electric Press Brake with DA66SThe E-Bend 3512 Servo Electric Press Brake is a compact and precise bending solution designed for modern sheet…View details
- Nouvelle presse plieuse MasterBend 20032 avec DA69SThe MasterBend 20032 New Press Brake is an advanced CNC bending solution designed for precision, productivity, and reliable…View details
- Presse plieuse hybride à double servomoteur MasterBend 13032The MasterBend 13032 Dual Servo Hybrid Press Brake is a high-performance CNC bending solution designed for precision sheet…View details
- Presse plieuse CNC robuste MasterBend 40080MasterBend 40080 is a high-performance CNC press brake designed for heavy-duty metal forming applications. With 400-ton bending force…View details
- Presse plieuse FlexBend 20032 pour pliage de précisionThe FlexBend 20032 Press Brake is a high-performance CNC bending machine designed for accurate and efficient sheet metal…View details
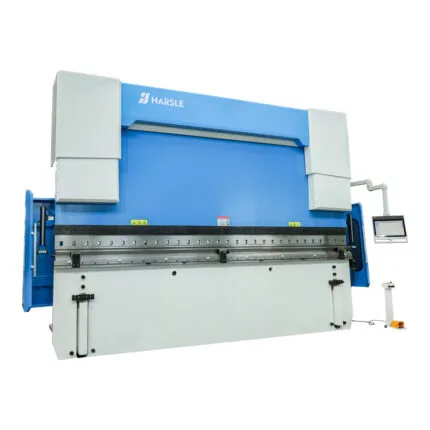
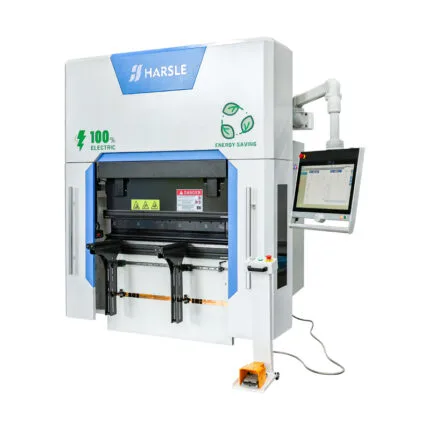
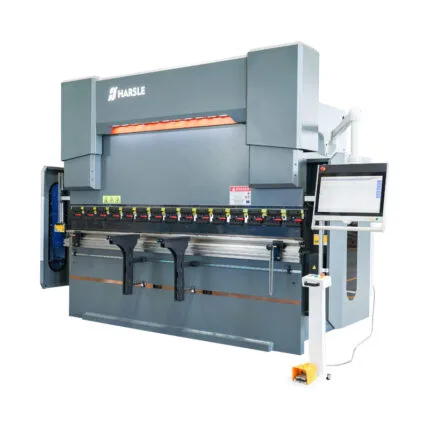

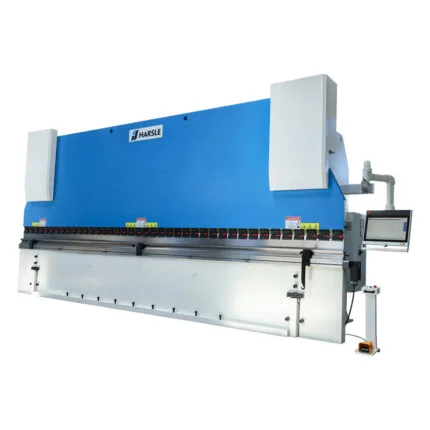
- Principaux fabricants chinois de machines de soudage laser pour l'industrieHARSLE is one of the leading China laser welding machine manufacturers, providing high-quality and cost-effective solutions for industrial…View details
- Machine de soudage laser à fibre 3 en 1 pour un travail de précisionThe 3 in 1 fiber laser welding machine integrates welding, cutting, and cleaning functions in one device. It…View details
- Machine de soudage laser haute efficacité 2 kW à vendreDiscover HARSLE’s 2KW laser welding machine, ideal for precise, high-speed metal joining. This powerful solution offers deep penetration,…View details
- Meilleurs fabricants de machines de soudage laser 1500 WDiscover top-tier 1500W laser welding machine manufacturers offering precision, efficiency, and durability. Ideal for metal fabrication, automotive, and…View details
- Fournisseurs fiables de machines de soudage laser 3000 WHARSLE is one of the leading 3000W laser welding machine suppliers, offering high-performance equipment for precise and efficient…View details
- Machine de soudage laser portable multifonction 5 en 1The 5 in 1 handheld laser welding machine offers welding, cutting, cleaning, polishing, and seam welding functions in…View details
- DualPolish 800 pour la finition des bords des pièces découpées au laserThe DualPolish 800 is a versatile deburring and chamfering machine designed specifically for laser-cut parts. With its precision…View details
- Machine de polissage et d'ébavurage magnétique pour pièces découpées au laserThe magnetic deburring polishing machine is specially designed for finishing sheet metal parts after laser cutting. It efficiently…View details
- Machines d'ébavurage de métaux plats pour le traitement des tôlesFlat metal deburring machines are designed to remove sharp edges, burrs, and slag from sheet metal parts after…View details
- Machine à ébavurer pour la finition des bords métalliquesThe deburring wheel machine is designed to efficiently remove burrs, sharp edges, and surface imperfections from metal parts…View details
- Machine d'ébavurage et de finition pour pièces métalliquesThe deburring and finishing machine is designed to remove sharp edges, burrs, and slag from metal parts after…View details
- Machine à chanfreiner les métaux à grande vitesseThe metal chamfering machine is designed for precise edge beveling and deburring of metal sheets and plates. It…View details
- Retourneur de panneaux de ligne de production pour la manutention de tôlesThe Production Line Panel Flipper is designed to improve efficiency and safety in sheet metal handling processes. It…View details
- Retourneur de panneaux de précision pour la manutention de tôlesThe Precision Panel Flipper is designed to improve efficiency and safety in sheet metal handling operations. It enables…View details
- Manipulateur de panneaux de fabrication pour l'automatisation de la manutention des métauxThe Fabrication Panel Handler is designed to improve efficiency and safety in sheet metal fabrication workflows. It automates…View details
- Solution intelligente de manutention de panneaux pour l'automatisation de la tôlerieThe Smart Panel Handling Solution is designed to improve efficiency and safety in modern sheet metal production lines.…View details
- Industrial Panel Flipping System for Metal FabricationThe Industrial Panel Flipping System is designed for efficient and safe handling of large sheet metal panels in…View details
- CNC Panel Flipper for Sheet Metal HandlingCNC Panel Flipper is an advanced sheet metal handling solution designed for safe, precise, and efficient panel rotation…View details
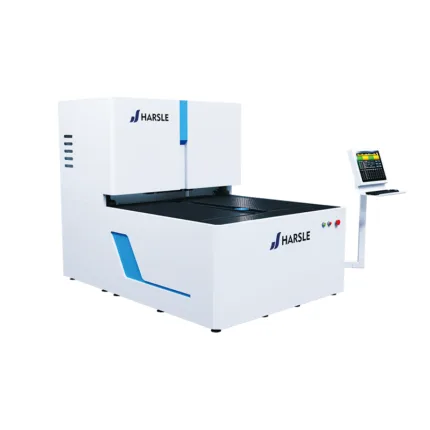
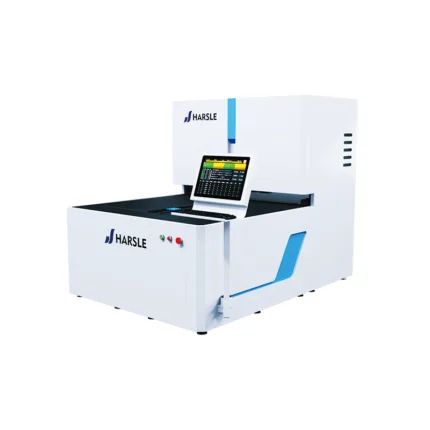
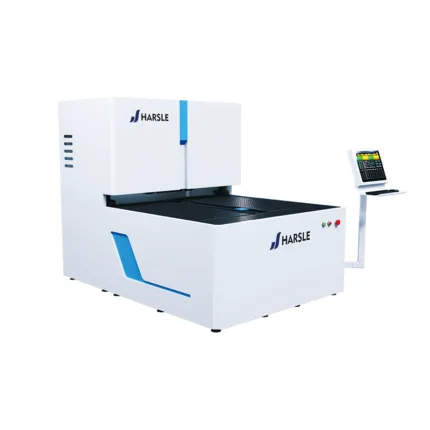
- Matrice réglable manuellement pour presse plieuseThe Manual Adjustable Die is a precision press brake tooling solution designed to improve bending accuracy and setup…View details
- Système de poinçonnage à poutre fixe à changement rapide pour presses plieusesThe Fixed-Beam Punch Quick-Change System is designed to significantly reduce tool setup time and improve bending efficiency for…View details
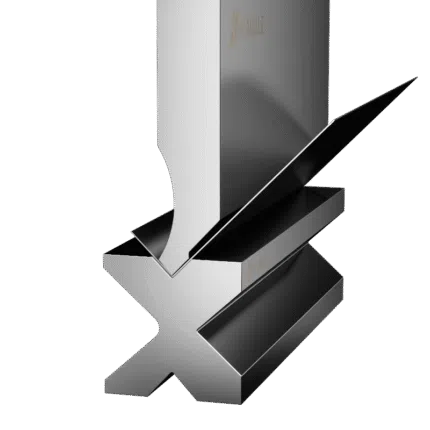
- Presse plieuse universelle 4 V pour pliage de tôlesHARSLE 4V Press Brake Die is designed for efficient and precise bending of metal sheets using CNC press…View details
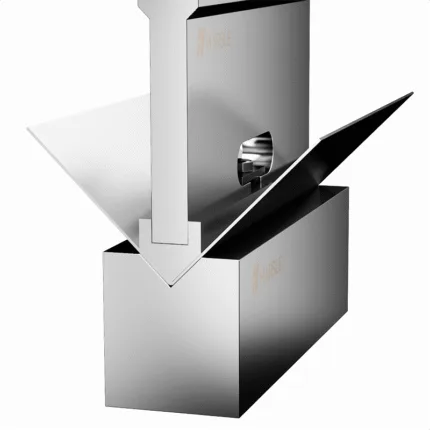
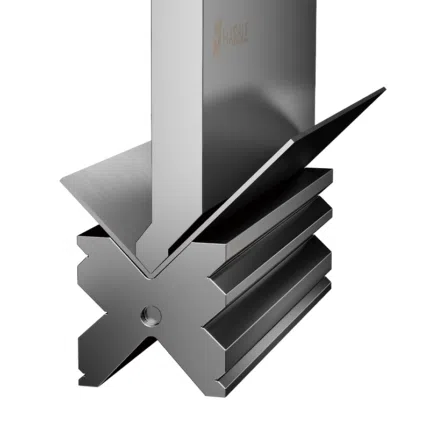
- Matrice multi-V et poinçon standard pour presse plieuseHARSLE's Multi-V Die and Standard Punch provide excellent versatility and precision for metal bending applications. Designed for press…View details
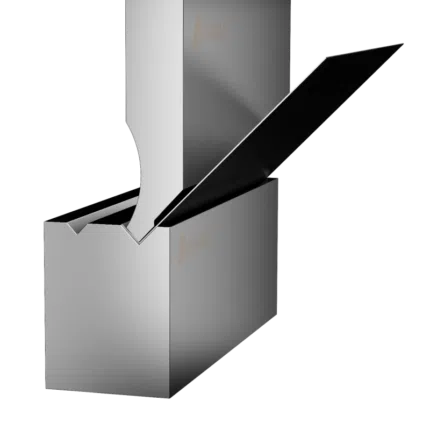
- Outil de poinçonnage standard de haute qualité pour un travail de précisionDiscover the Standard Punch Tool designed for precision and durability in metal fabrication. Engineered for accurate punching operations,…View details
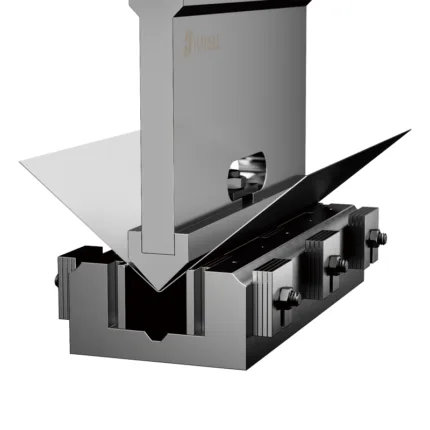
- Ensemble de poinçons et matrices d'ourlet de haute précisionEnhance your sheet metal fabrication with our High-Precision Hemming Punch and Die Set. Designed for accuracy and durability,…View details
Challenges & Solutions
What Matters in Elevator Manufacturing
No scratches on decorative stainless
Panel benders keep the sheet supported on brushes; polyurethane film and dedicated tooling protect the face on press brakes.
Sharp, small-radius edges
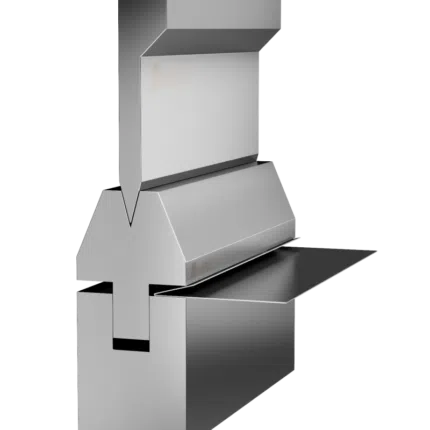
V-grooving before bending gives the crisp edges architects specify for car doors and wall panels.
Straight flanges over 2–3 m
Crowning on CNC press brakes and the rigid frame of a panel bender keep angles constant over the full length.
Invisible welds
Laser welding of stiffeners leaves little or no mark on the visible side.
Automate Bending
Panel Bender for Elevator Manufacturing
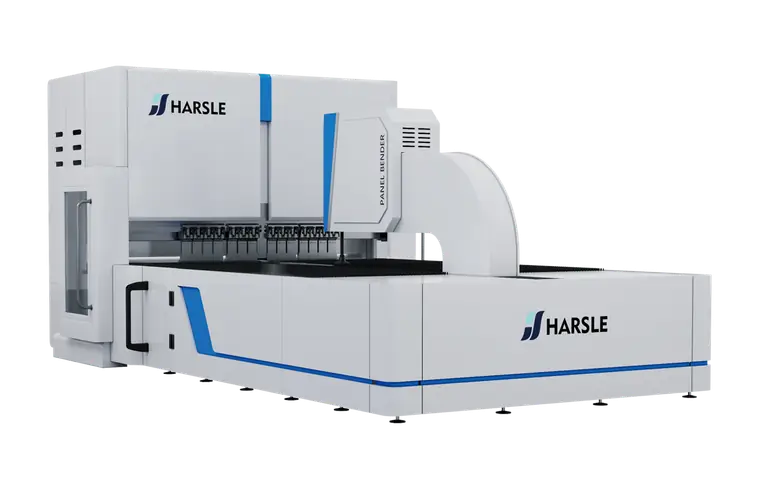
A HARSLE panel bender clamps the sheet flat and forms all four sides in one cycle with universal tooling — ideal for the repeat panels, doors and boxes found in elevator doors & cabins.
- Bending length 1400–3000 mm (AutoBend)
- 0–180° bending angle, 0.2 s per bend
- Minimal operator skill, fast changeovers
Empreinte mondiale
Shipments & Customer Stories
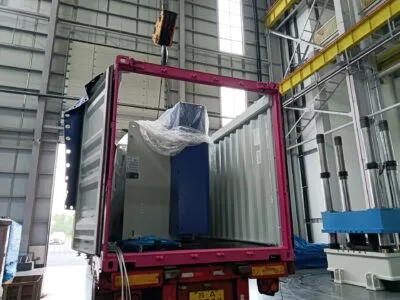
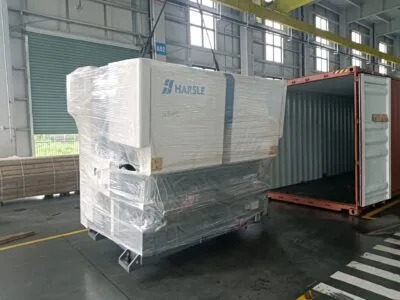
Every shipment and customer story HARSLE publishes appears here automatically. Filter by machine or country.
- 1,209Shipments published
- 118Destination countries
- 118Customer stories
- LiveUpdated as we ship
![UAE-Flexbend 25050 Press Brake]() ShippedUAE-Flexbend 25050 Press Brake
![Iran-Flexbend8032 Press Brake]() ShippedIran-Flexbend8032 Press Brake
![Mexico-MasterBend 20040 Press Brake]() ShippedMexico-MasterBend 20040 Press Brake
![Australia-PrimeShear 0632 Guillotine Shear With feeding table]() ShippedAustralia-PrimeShear 0632 Guillotine Shear With feeding table
![USA-Masterbend 30050 Press Brake]() ShippedUSA-Masterbend 30050 Press Brake
![USA-MasterBend 20032 Press Brake]() ShippedUSA-MasterBend 20032 Press Brake
![Brazil-Masterbend 17032 CNC Press Brake]() ShippedBrazil-Masterbend 17032 CNC Press Brake
![Russia-TiltPunchJ21-200T Punching Machine]() ShippedRussia-TiltPunchJ21-200T Punching Machine
![Ireland-QuadRoll 2516 Rolling Machine]() ShippedIreland-QuadRoll 2516 Rolling Machine
![USA-DualPolish DMV1000 Deburring Machine]() ShippedUSA-DualPolish DMV1000 Deburring Machine
![Machine à rouler Guatemala-QuadRoll 1630]() ShippedMachine à rouler Guatemala-QuadRoll 1630
![Presse plieuse CNC Serbia-MasterBend 6332]() ShippedPresse plieuse CNC Serbia-MasterBend 6332
![Presse plieuse électrique USA-E-Bend Pro 7025]() ShippedPresse plieuse électrique USA-E-Bend Pro 7025
![Presse plieuse Brazil-Flexbend 17032]() ShippedPresse plieuse Brazil-Flexbend 17032
![Presse plieuse CNC Zimbabwe-FlexBend 300T4000]() ShippedPresse plieuse CNC Zimbabwe-FlexBend 300T4000
![Cisaille guillotine Brazil-PrimeShear 0860]() ShippedCisaille guillotine Brazil-PrimeShear 0860
![Presse plieuse hydraulique Argentina-EasyBend 8032]() ShippedPresse plieuse hydraulique Argentina-EasyBend 8032
![Presse plieuse CNC USA-MasterBend 17040]() ShippedPresse plieuse CNC USA-MasterBend 17040
![Cisaille guillotine PrimeShear 1232, Suisse]() ShippedCisaille guillotine PrimeShear 1232, Suisse
![Presse plieuse CNC Venezuela-Ecobend 17025]() ShippedPresse plieuse CNC Venezuela-Ecobend 17025
![Cisaille à guillotine mécanique Indonésie-Q11D-13X2500]() ShippedCisaille à guillotine mécanique Indonésie-Q11D-13X2500
![Presse plieuse CNC Algérie-Ecobend 6325]() ShippedPresse plieuse CNC Algérie-Ecobend 6325
![Presse plieuse CNC Finland-Flexbend 80T2000]() ShippedPresse plieuse CNC Finland-Flexbend 80T2000
![Cintreuse de panneaux Brésil-Autobend 2000]() ShippedCintreuse de panneaux Brésil-Autobend 2000
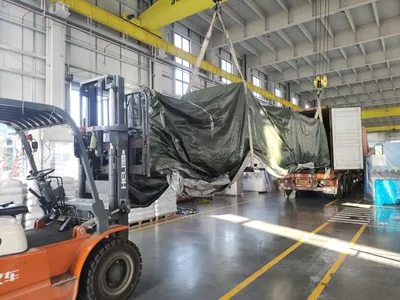
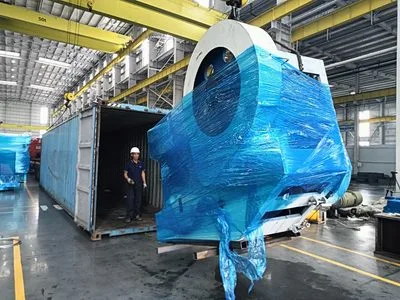
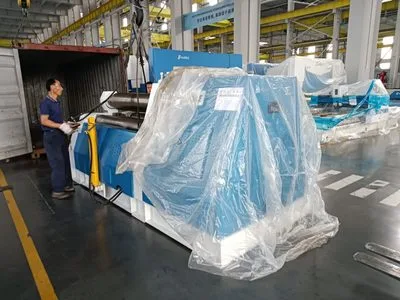
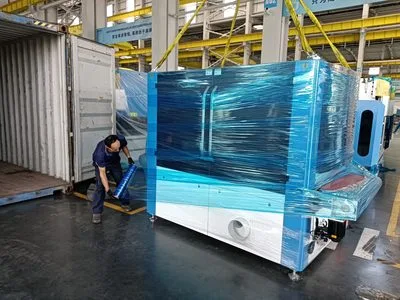
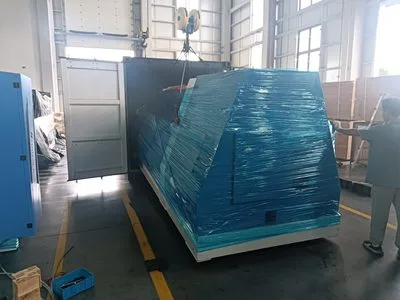
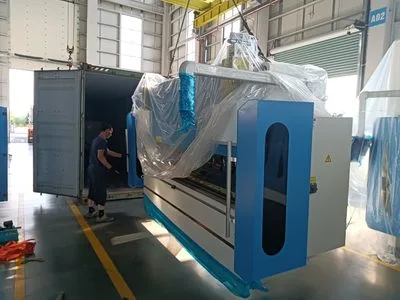
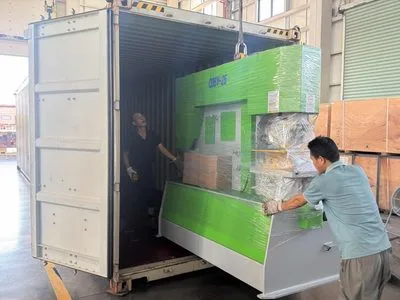
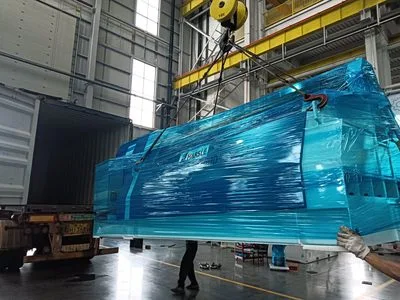
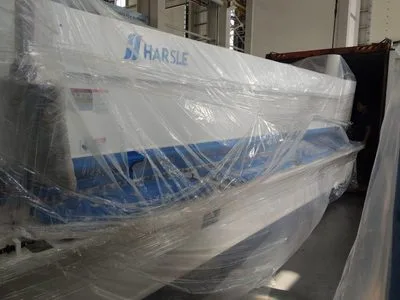
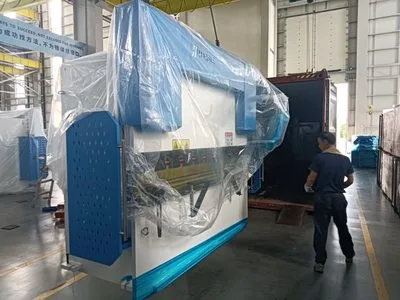
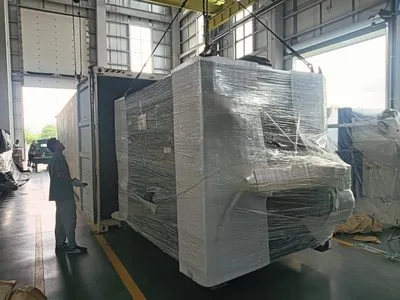
No shipments match this filter yet.
![HARSLE Press Brake Software Upgrade Unlocks US Client Potential]() StoryHARSLE Press Brake Software Upgrade Unlocks US Client Potential
![HARSLE Panel Bender Fast Setup Wins United States Praise]() StoryHARSLE Panel Bender Fast Setup Wins United States Praise
![HARSLE Tube Bending Machine Training Boosts Thailand Output]() StoryHARSLE Tube Bending Machine Training Boosts Thailand Output
![HARSLE Engineer Support Wins United States Client Praise]() StoryHARSLE Engineer Support Wins United States Client Praise
![L'assistance d'ingénieurs sur site permet de conclure un accord à long terme au Liban.]() StoryL'assistance d'ingénieurs sur site permet de conclure un accord à long terme au Liban.
![Un client libanais salue la qualité de la presse plieuse HARSLE]() StoryUn client libanais salue la qualité de la presse plieuse HARSLE
![Une machine à tordre conforme aux normes CSA ravit un client canadien]() StoryUne machine à tordre conforme aux normes CSA ravit un client canadien
![Test d'acceptation en usine réussi pour un client chilien]() StoryTest d'acceptation en usine réussi pour un client chilien
![Une solution de pliage à haut rendement améliore la production en Grèce]() StoryUne solution de pliage à haut rendement améliore la production en Grèce
![Livraison de cintreuses de tubes en douceur pour un client de Séville]() StoryLivraison de cintreuses de tubes en douceur pour un client de Séville
![Un client de Séville félicite le service technique de la presse plieuse]() StoryUn client de Séville félicite le service technique de la presse plieuse
![Un client américain félicite HARSLE pour son service d'installation professionnel.]() StoryUn client américain félicite HARSLE pour son service d'installation professionnel.
![L'Arizona approuve les performances supérieures des machines HARSLE]() StoryL'Arizona approuve les performances supérieures des machines HARSLE
![Les machines HARSLE font le bonheur du Liban grâce à leurs hautes performances.]() StoryLes machines HARSLE font le bonheur du Liban grâce à leurs hautes performances.
![Succès à Sioux Falls : Production accrue grâce à HARSLE]() StorySuccès à Sioux Falls : Production accrue grâce à HARSLE
![Succès de la machine HARSLE auprès d'un client fidèle aux États-Unis]() StorySuccès de la machine HARSLE auprès d'un client fidèle aux États-Unis


No stories match this filter yet.
Knowledge Center
Elevator Manufacturing Guides
FAQ
Questions fréquemment posées
Common questions about machines and processes for elevator doors & cabins.
Which machines are used to make elevator doors?
A typical elevator door line uses a shear or fiber laser for blanks, a V-grooving machine for sharp edges, a panel bender or long CNC press brake for folding, laser welding for stiffeners and a deburring or polishing step.
Why is V-grooving used for elevator panels?
Cutting a V-groove on the bend line reduces the material left at the corner, so the bend has a very small outside radius. This gives the sharp, architectural edge required on car doors and cabin panels.
Panel bender or press brake for elevator doors?
A panel bender folds long doors with less handling and fewer surface marks and is ideal for repeat sizes. A long or tandem CNC press brake is more flexible for frames, jambs and very long parts.
How do you prevent scratches on stainless elevator panels?
Keep the protective film on during cutting and bending, use brush tables and film-protected tooling, and avoid sliding the sheet across steel surfaces.
What thickness are elevator panels?
Car doors, landing doors and cabin walls are mostly 1.0–1.5 mm stainless or coated steel; frames and jambs are typically 1.2–2.0 mm.
More Applications
Other Industries We Equip
 Electrical Enclosures & Cabinets
- HVAC Equipment & Ductwork
 Commercial Kitchen & Food Service Equipment
 Office & Metal Furniture
- Medical & Laboratory Equipment
- Automotive Parts & Vehicles
- Composants aérospatiaux
- Shipbuilding & Marine
 Construction, Facades & Interiors
- Home Appliances
- Sheet Metal Fabrication & Job Shops
- Signage, Advertising & Displays
- Tube & Pipe Processing
- Pressure Vessels, Tanks & Oil and Gas
 Wind, Solar & Power Equipment
 Heavy Machinery & Agricultural Equipment
- Production Line Solutions
Commencer
Demander un devis
Tell us about your elevator doors & cabins — our engineers will recommend the machines and layout.
- Sélection de machinesModel, series and options matched to your parts
- Support techniqueBend feasibility checked on your drawings
- Devis détailléPrice, lead time, shipping and installation
- Réponse en 24 heuresA real engineer replies within one business day
Tip: mention your material, thickness, largest part size and yearly volume for the most accurate quote.


